
 EN



For wire EDM jobs, the practical route to reducing waste is to plan a workable stock layout, check the actual cut width and support the parts through the cutting sequence. Confirm savings by comparing the stock required for the same accepted output. A thin wire or a tightly packed drawing alone does not demonstrate a saving.
Define the stock and accepted output
Begin with the material grade and condition, usable stock dimensions, part drawing revision, quantity and inspection requirements. Compare the existing and proposed layouts for the same accepted output. Changing the part specification or counting unfinished blanks as finished parts makes the comparison misleading.
- Record the stock issued to the job, including any material reserved for clamping or locating.
- Count accepted parts separately from rejects and parts awaiting inspection or rework.
- Identify material removed in cutting and any subsequent processing within the agreed route.
- Record retained offcuts separately from unusable remainder. A retained piece is not automatically suitable for another job.
Use a consistent basis, such as mass or volume, for the stock and part-material comparison. Keep recovered material, rejected output and processing losses separate so they are not counted twice. If reclaimed stock is included, record its origin, usable dimensions and condition rather than treating it as an equivalent new blank.
Separate wire diameter from the actual cut width
Wire EDM removes material through electrical discharges between an electrode wire and an electrically conductive workpiece. It is a non-contact cutting process, not a mechanical saw. Conductivity is an initial eligibility condition; the specific material, condition, geometry and acceptance requirements still need review.
Do not use wire diameter as the measured width of the finished cut. Confirm the proposed machine, wire, working fluid, cutting sequence and programmed compensation. Request actual measurements for the relevant material and feature before assigning spacing or allowances. A result from a different machine or setup does not establish the cut width of your job.
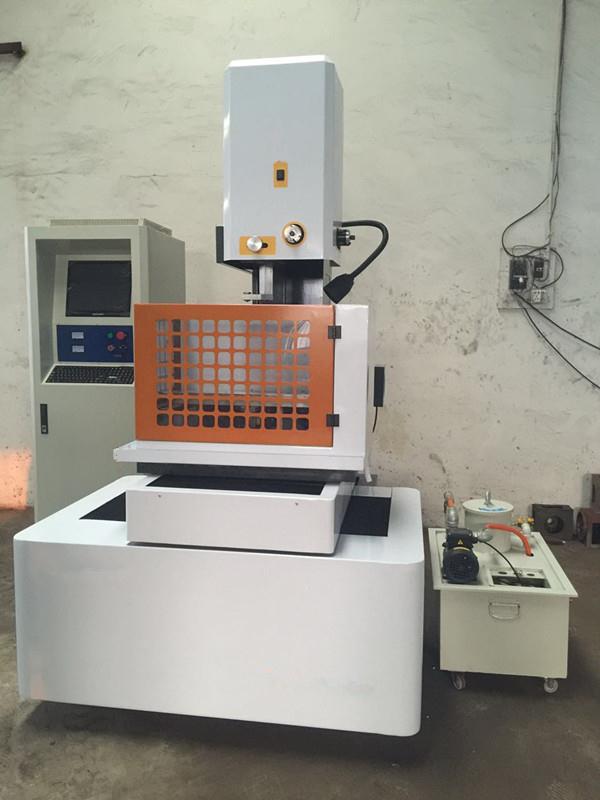
Check a layout that can actually be cut
- Mark the usable stock boundary, clamping areas, datums and any regions that must remain clear.
- Check the complete wire path and entry arrangement for each contour. Confirm start-hole or edge access where applicable.
- Plan part and core support, any retained bridges and the cutting order before releasing a contour.
- Check the proposed spacing and machining allowances against the qualified cutting route and required finished dimensions.
- Review whether the remaining stock or removed cores can be identified, inspected and used for an actual later requirement.
A nesting or program preview can help review the plan, where the supplied software supports it. It does not prove that the workholding, cutting sequence or finished parts will pass inspection. Verify the installed software and axis functions rather than assuming every machine has specialised nesting or that more axes eliminate additional setups.
Include surface acceptance and the complete route
Non-contact cutting does not mean the surface is unaffected by heat. EDM may leave a recast layer or heat-affected zone. Define any relevant surface-integrity requirement and acceptance method for the part; neither universal zero-heat claims nor an assumed mandatory finishing allowance is appropriate.
Include preparation, cutting stages, handling, inspection and any agreed later processing in the comparison. Decide whether finishing or further machining is needed from the drawing and accepted result, not from a general near-net-shape claim. A layout that uses less stock but produces unacceptable parts has not demonstrated a usable improvement.
Record losses during a representative job
For a trial or repeat job, record the material lot, drawing revision, machine configuration, setup and cutting route alongside accepted output. Note interruptions, rejected parts, rework and the reasons for each. Keep estimates separate from measured results and state which activities the record includes.
Follow the manufacturer's instructions for the actual equipment and consumables. Agree who checks setup condition and records changes before comparing jobs. Distinguish available machine logs from operator observations and inspection results; do not assume automatic monitoring, calibration or maintenance guarantees fewer rejected parts.
Common questions about material use
Does tighter nesting always reduce waste
No. The layout still needs workable access, support, spacing and a cutting sequence that meets the part requirements. Compare actual accepted output and retained material, not just the occupied area in a software preview.
Is wire EDM always less wasteful than laser cutting
No universal ranking is justified. Compare the same material, drawing, quantity and acceptance criteria through the complete processing route. Different cut widths, edge requirements, rejected parts and later operations can change the result. Use the separate Wire EDM vs laser cutting selection guide for the broader process decision.
Can material savings alone establish a payback period
They are not a complete investment assessment. Use actual material spending and accepted production, then account for equipment, programming, workholding, labour, consumables, maintenance, inspection and any later operations. State the assumptions and compare estimates with measured results. There is no universal payback period to apply to a machine purchase.
What to send for a material-use review
- The drawing revision and units, required quantity and accepted-part specification.
- The exact material grade and condition, stock dimensions, thickness and weight.
- The current layout and proposed layout, including wire entry, clamping, support and cutting order.
- Required dimensions, surface finish and any surface-integrity checks, with the measurement method.
- Available records of stock used, accepted and rejected parts, rework and retained offcuts.
- The proposed machine or functions needed, power supply and destination country.
Include these details with your machine enquiry and ask which assumptions, configuration items and sample results need confirmation. If a saving is quoted, ask for its material, quantity and accepted-part basis rather than relying on a generic percentage.
Manufacturer documentation
The FANUC Wire Cutting EDM explanation describes the basic discharge and non-contact mechanism. Makino's UPN-01 release illustrates that wire diameter and finished slot width are different in a particular micro-machining setup. Makino's aerospace EDM webinar summary notes possible recast and heat-affected-zone concerns. These documents do not establish HarsMarg machine specifications, a universal cut-width formula or material-saving results.
Table of Contents
- Define the stock and accepted output
- Separate wire diameter from the actual cut width
- Check a layout that can actually be cut
- Include surface acceptance and the complete route
- Record losses during a representative job
- Common questions about material use
- What to send for a material-use review
- Manufacturer documentation
