
 EN




The main applications of electrical discharge machining (EDM) are cutting profiles in electrically conductive material, forming blind or three-dimensional cavities, and producing small or deep holes that are difficult to make by conventional cutting. These tasks use different machine types: Wire EDM for profile cutting, die-sinking EDM for shaped cavities and EDM drilling for holes made with a tubular electrode.
Choosing the correct process matters more than attaching an industry name to the job. A part described as “aerospace,” “medical,” “automotive” or “electronics” does not automatically belong on one EDM machine. The material must be electrically conductive, the feature must suit the electrode and dielectric path, and the required size, roughness, surface integrity and inspection method must be confirmed for the actual machine and setup.
EDM Process Comparison at a Glance
| Process | Electrode and Motion | Best-Matched Feature | Main Selection Questions |
|---|---|---|---|
| Wire EDM | A moving wire electrode follows a programmed or controlled cutting path through the workpiece | Through-profiles, punches, dies, inserts, slots and cut-off features | Work envelope, thickness, taper, start/through access, wire architecture, cut sequence, tolerance and finish |
| Die-sinking EDM | A shaped electrode advances into the workpiece across a controlled spark gap | Blind cavities, ribs, pockets, internal details and three-dimensional forms | Cavity depth/area, electrode material and count, wear allowance, flushing, surface texture, integrity and axis/control needs |
| EDM drilling | A tubular electrode normally rotates while dielectric is delivered through the electrode | Small or deep holes, start holes and localized conductive features | Electrode range, hole size/depth/angle, material, breakthrough, flushing, position tolerance and axis/automation needs |
One machine should not be assumed to perform all three processes. Hybrid or option-equipped machines exist in the wider market, but the available function must be confirmed on the exact model and quotation.
What All EDM Processes Share—and What They Do Not
EDM removes material through controlled electrical discharges across a dielectric-filled machining gap. The workpiece therefore needs sufficient electrical conductivity for the intended process. Because material is eroded thermally instead of being sheared by a conventional cutting edge, hardness alone is not the deciding limit. Hardened steels, conductive carbides and many conductive alloys may be candidates when the geometry and process conditions are suitable.
“Non-contact” does not mean “no process effect.” EDM can leave a recast or white layer and other heat-affected surface features. Electrode wear, wire behavior, debris removal, dielectric condition and thermal stability can influence dimensions and finish. Safety-critical or regulated parts therefore need a drawing-based process qualification and inspection plan rather than a generic precision claim.
The dielectric arrangement also differs. Do not import water-resistivity, ion-exchange, filter, additive or maintenance guidance from one EDM type to another without checking the exact machine and fluid documentation.
Wire EDM Applications: Profiles, Inserts and Through-Cuts
Wire EDM machines are selected when a wire can pass through or start inside an accessible hole and follow the required contour. Typical feature-level applications include punch and die profiles, mold inserts, gauges, conductive plates, narrow slots, extrusion or forming-tool profiles, and removal of a component from conductive stock.
The wire path creates a kerf and normally produces a through-cut; it does not replace die-sinking EDM for a blind three-dimensional cavity. The available taper, workpiece thickness, load, wire diameter/type, flushing, cut count and controller strategy must be reviewed for the actual model. HarsMarg currently separates reciprocating Wire EDM into single-cut machines and multi-cut machines; consumable and setup assumptions from continuously fed brass-wire equipment should not be copied to these machines without model verification.
For a broader explanation of process benefits and limits, see the HarsMarg Wire EDM advantages guide.
Die-Sinking EDM Applications: Blind Cavities and Shaped Details
Die-sinking EDM is selected when a shaped electrode must reproduce a cavity or internal feature that a wire cannot create. Common examples include mold cavities, ribs, pockets, logos, internal corners and localized forms in electrically conductive workpieces. Electrode manufacture, undersize, polarity, roughing/finishing stages, wear allowance, dielectric circulation and debris escape are part of the process plan.
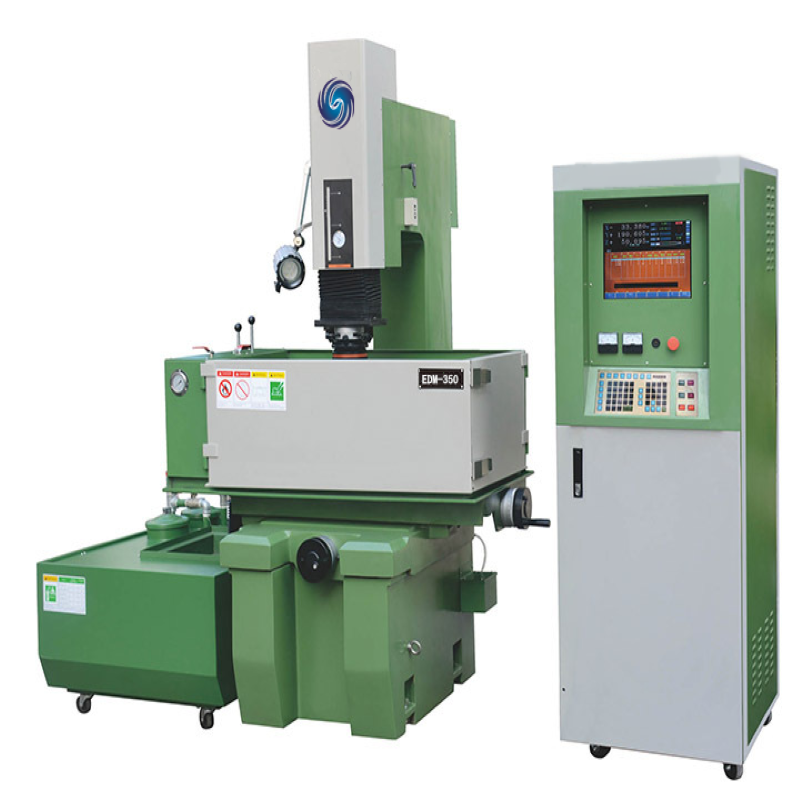
Choose between ZNC die-sinking EDM and CNC die-sinking EDM from the required motion/control, electrode and workpiece envelope, table load, cavity geometry, process stages and automation needs—not from a generic surface-finish promise.
EDM Drilling Applications: Start Holes and Small or Deep Holes
EDM drilling machines commonly use a rotating tubular electrode and internal dielectric flushing. They are considered for start holes used by Wire EDM, small or deep holes in conductive tooling and parts, and features where conventional drills face access, hardness or tool-force limitations.
Electrode diameter is not automatically the guaranteed finished-hole diameter. The final hole depends on overcut, electrode wear, material, depth, angle, flushing, entry/exit condition and machine setup. Position, roundness, taper, recast layer and breakthrough damage may need separate inspection. See the EDM drilling applications and machine-selection guide for the current D703/DD703 boundary.
Industry Examples Must Be Matched to the Feature
EDM is used across die and mold, general precision manufacturing, aerospace/energy, medical, automotive and electronics supply chains. The useful question is not “Does this industry use EDM?” but “Which conductive feature, on which material, with which acceptance criteria, suits which EDM process?”
| Application Family | Potential EDM Tasks | Important Validation Boundary |
|---|---|---|
| Die and mold / tooling | Wire-cut punches, die openings and inserts; sunk cavities, ribs and internal details; drilled start or vent holes | Fit, clearance, taper, corner radius, cavity finish, electrode/wire strategy and tool-steel condition |
| Aerospace and energy supply chain | Conductive profiles, difficult localized features and cooling/film-hole work where the selected EDM type is suitable | Approved material/process route, feature geometry, recast/heat-affected condition, inspection, traceability and customer qualification |
| Medical and precision instruments | Conductive tooling and selected conductive-component profiles, cavities or holes | Regulatory/customer approval, biocompatibility route, cleaning, surface integrity, burr/edge condition and validated inspection; EDM alone proves none of these |
| Automotive and general manufacturing | Injection or forming tooling, conductive precision profiles, cavities and selected small-hole features | Cycle time, lot size, tool/electrode cost, inspection, automation and comparison with milling, grinding, laser or conventional drilling |
| Electronics and semiconductor tooling | Precision mold/die inserts, lead-frame or trim/form tooling and selected conductive features | Actual feature size, material conductivity, contamination controls, tool life, inspection and required machine capability |
These examples do not establish that one HarsMarg model meets a regulated-industry requirement. A model-specific quotation and, where necessary, a representative sample test are required.
When EDM May Not Be the Best Process
EDM should be compared with other processes when:
- the workpiece is not sufficiently electrically conductive under the intended conditions;
- the feature is a simple open shape that can be removed more economically by milling, turning, grinding, sawing or drilling;
- the required geometry does not provide a suitable wire path, electrode approach or dielectric/debris path;
- the permitted recast layer, microcracking, thermal effect or surface condition cannot be met by the qualified process and any approved post-process;
- the part envelope, load, feature depth or access exceeds the verified machine configuration;
- the required throughput or total cost favors another validated method.
A good machine-selection review compares the complete route: electrode or wire, setup, roughing/finishing passes, inspection, post-processing, consumables, maintenance, throughput and operator requirements.
Information to Send for EDM Process Selection
To receive a useful technical response, send:
- a 2D drawing or 3D model identifying the exact feature to be machined;
- workpiece material, grade, hardness/condition, dimensions and weight;
- whether the feature is a through-profile, blind cavity or hole, including depth, angle, taper and access;
- dimensional tolerance, Ra/Rz, edge condition and any recast-layer or microcrack limit;
- inspection standard, measurement method and any customer or regulated-process approval;
- lot size, cycle-time target, current process and observed problem;
- required axes, taper/orbit/jump or automation functions, but only if the application needs them;
- destination country, available power supply and site requirements.
If the requirement is close to a machine limit or includes a critical surface-integrity criterion, define a representative sample and acceptance plan before purchase. The test should state material, geometry, electrode or wire, process sequence, measurement locations/methods and the result that will constitute acceptance.
Frequently Asked Questions
Can EDM machine any metal?
EDM requires an electrically conductive workpiece. Conductivity is necessary but does not guarantee that every material, size or feature is practical. Geometry, dielectric and debris access, thermal effects, machine capacity, required quality and economics still need review.
Can one EDM machine cut profiles, sink cavities and drill holes?
Do not assume so. Wire EDM, die-sinking EDM and EDM drilling use different electrodes, motion and fluid delivery. Some market machines have special or hybrid functions, but the exact capability must be listed in the model configuration and quotation.
Can Wire EDM make a blind cavity?
A conventional Wire EDM path normally produces a through-cut because the wire passes through the workpiece. A blind three-dimensional cavity is generally a die-sinking EDM task.
Does EDM guarantee high accuracy or a fine surface?
No generic process name guarantees a result. Accuracy and finish depend on the machine/configuration, electrode or wire, workpiece, geometry, setup, process stages, dielectric/debris control, thermal state and measurement method. Use the model specification and a representative qualification test where required.
Is EDM only useful for very hard material?
No. EDM is often chosen for hardened or difficult-to-cut conductive material, but hardness is not the only reason. Feature geometry, cutting force, tool access, required detail and the overall validated process route may make EDM useful on other conductive materials as well.
How should an EDM application be confirmed before buying a machine?
Match the required feature to the correct EDM process, check the verified model envelope and functions, then document the material, geometry, tolerance, surface requirement, inspection and production needs. For critical or borderline work, agree on a representative sample test and acceptance method.
Request an EDM Application Review
Send HarsMarg your drawing, material, feature type, workpiece size/weight, tolerance, surface and integrity requirements, lot size, automation needs, power supply and destination. We can route the inquiry to the relevant Wire EDM, die-sinking EDM or EDM drilling family and identify which capability must be confirmed in the technical quotation. Submit your EDM application for review.
Table of Contents
- EDM Process Comparison at a Glance
- What All EDM Processes Share—and What They Do Not
- Wire EDM Applications: Profiles, Inserts and Through-Cuts
- Die-Sinking EDM Applications: Blind Cavities and Shaped Details
- EDM Drilling Applications: Start Holes and Small or Deep Holes
- Industry Examples Must Be Matched to the Feature
- When EDM May Not Be the Best Process
- Information to Send for EDM Process Selection
- Frequently Asked Questions
- Request an EDM Application Review
