
 EN



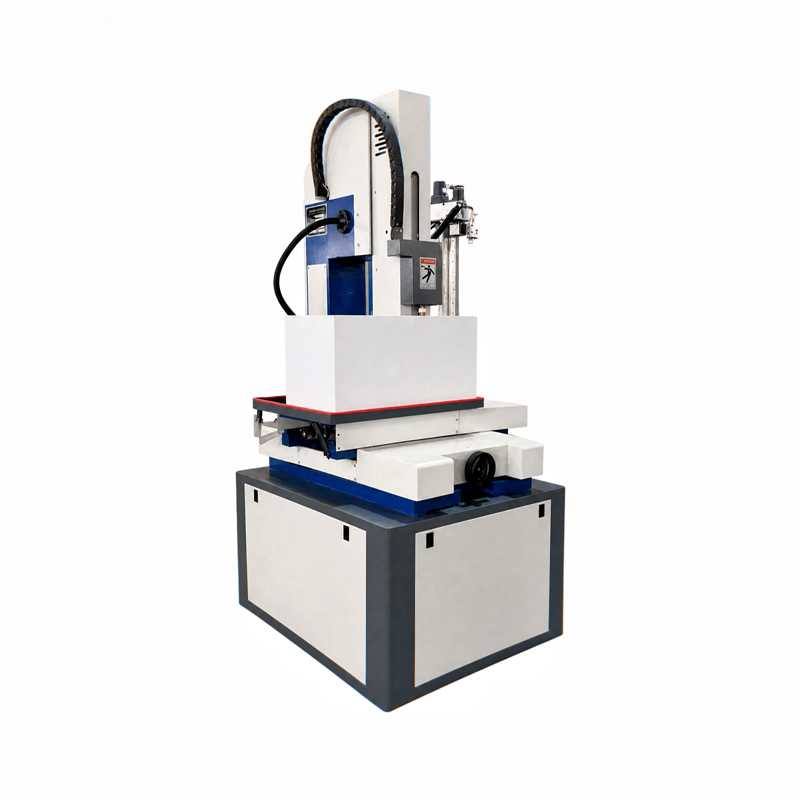
EDM hole drilling is commonly used to produce small or deep holes, Wire EDM start holes, process holes and repeated coordinate hole patterns in electrically conductive workpieces. It is especially worth evaluating when a material, hole diameter or drilling depth makes conventional cutting difficult. The process is not suitable for a nonconductive workpiece, and no machine should be selected from the process name alone: material grade, hole geometry, tolerance, quantity, flushing conditions and inspection requirements must all be reviewed.
For HarsMarg equipment, the D703 is a non-CNC machine with controlled Z-axis feed, while the DD703 is the CNC/multi-axis option for programmed coordinate positioning. Both current product pages list an electrode-diameter range of φ0.3–φ3.0 mm. That is an electrode range—not a guaranteed finished-hole range—and the final hole must be assessed from the actual part and process.
How Does EDM Hole Drilling Work?
EDM hole drilling removes material through controlled electrical discharges between an electrode and an electrically conductive workpiece. A tubular electrode is commonly rotated while working fluid passes through it to carry eroded material away from the discharge area and help maintain a stable gap. Because material is removed by electrical discharge rather than a conventional cutting edge, the process can be evaluated for hardened conductive components and for hole geometries that are difficult for a mechanical drill.
The process still has practical limits. Electrical conductivity is essential, and results depend on the workpiece grade, electrode specification, hole diameter and depth, flushing access, electrical settings, machine configuration, setup and measurement method. Material hardness alone does not determine suitability or cycle time. Because EDM is a thermal process, recast-layer and heat-affected-zone requirements should be defined and inspected when they matter to the part.

| Application Question | Why EDM Drilling May Be Considered | What Must Be Confirmed |
|---|---|---|
| Is the workpiece electrically conductive? | Electrical discharge requires a conductive path through the workpiece. | Exact material and grade; do not assume suitability from a broad material family. |
| Is the hole small, deep or difficult to reach with a conventional drill? | A tubular electrode and internal working-fluid flow can support debris removal in demanding hole geometries. | Hole diameter, depth, entry location, surrounding clearance and through-hole or blind-hole requirement. |
| Is a Wire EDM start hole required? | EDM drilling can create a start passage through which the Wire EDM electrode wire is threaded. | Wire-threading clearance, start position, workpiece thickness and the following Wire EDM cut plan. |
| Does the part contain a repeated hole pattern? | A CNC/multi-axis configuration can be reviewed for programmed coordinate positioning. | Hole count, coordinates, pitch, datum, positional tolerance and production quantity. |
| Are speed, finish or tolerance critical? | EDM drilling may fit the geometry, but the required result must be demonstrated under defined conditions. | Acceptance values, representative material, electrode, depth, settings, flushing and inspection method. |
Common EDM Drilling Applications
1. Start Holes for Wire EDM
A start hole provides the path needed to thread the Wire EDM electrode wire before cutting a closed internal contour. Typical examples include internal openings, slots or profiles that do not begin from an outside edge. The required start-hole position and diameter should be determined from the Wire EDM wire size, threading method, contour and workpiece thickness.
EDM hole drilling and Wire EDM are separate processes. The drilling machine prepares the start passage; the Wire EDM machine then cuts the programmed profile. Calling the first operation “Wire EDM drilling” can confuse the equipment and process requirements.
2. Process Holes in Tool, Die and Mold Components
Tool, die and mold components may require start holes, vent holes, flushing holes, ejector-related holes or other straight process holes in hardened conductive material. EDM drilling can be reviewed when conventional drilling is limited by material condition, small diameter or depth. The drawing must still define the entry point, final diameter, depth, position and any surface or recast-layer acceptance requirement.
Do not assume that every cooling-channel geometry can be produced by a standard EDM drilling setup. Intersecting, angled, blind or multi-direction passages require a specific machine and fixture review before they are quoted.
3. Cooling, Flow and Orifice Holes in Conductive Metal Parts
Cooling or flow holes in conductive alloy components are established industry uses of EDM drilling. Candidate parts may occur in turbine, energy, hydraulic, fuel-control or other thermal and flow-management systems. These examples describe the process category; they do not establish that a particular HarsMarg machine has already been qualified for an aerospace, medical, automotive or regulated component.
For a technical review, provide the exact alloy, hole diameter and depth, entry angle, wall thickness, hole count, required flow or dimensional acceptance, and inspection method. A successful hole-making trial does not by itself certify the finished component or its performance in service.
4. Repeated Coordinate Hole Patterns
Plates, inserts, nozzles, fixtures and similar conductive components may require multiple holes at programmed coordinates. This application should be evaluated from the datum, coordinate list, spacing, positional tolerance and part quantity—not simply from the number of machine axes. A CNC/multi-axis configuration such as the DD703 is the relevant starting point when repeated coordinate positioning is required.
5. Small or Deep Holes in Hardened Conductive Materials
EDM drilling may be considered for hardened steels and other electrically conductive grades when a conventional drill is unsuitable or difficult to control. The material must be identified by its actual grade because conductivity, composition, heat treatment and flushing behavior can change the process. No universal drilling speed, depth-to-diameter ratio, accuracy or surface finish should be applied across different materials and hole geometries.
| Application | Typical Decision Driver | Information Needed Before Quotation | Important Limitation |
|---|---|---|---|
| Wire EDM start hole | Closed internal contour requiring wire access | Wire size, start position, workpiece thickness and contour drawing | The drilled hole and the following Wire EDM operation are separate processes. |
| Tool, die or mold process hole | Hardened conductive material or a difficult small/deep feature | Material grade, diameter, depth, position and section drawing | Complex channels or special angles require a confirmed configuration. |
| Cooling or flow hole | Small passage in a conductive alloy component | Alloy, diameter, depth, angle, wall section and inspection criteria | No industry qualification, flow performance or service life is implied. |
| Repeated coordinate pattern | Multiple holes positioned from a defined datum | Coordinate list, pitch, tolerance, quantity and fixture concept | Command increment is not the same as achieved positional accuracy. |
| Small or deep hole in hardened material | Conventional-drilling difficulty | Exact grade, heat treatment, diameter, depth and required result | No universal aspect ratio, cycle time or hole-quality claim applies. |
How Should You Choose Between D703 and DD703?
Choose the control arrangement first, then confirm physical capacity. The D703 is intended for a simpler non-CNC drilling setup with controlled Z-axis feed. The DD703 is the CNC/multi-axis option when a project requires programmed coordinate positioning or repeated hole patterns. Published travel or table size does not establish hole accuracy, and an electrode range does not establish a finished-hole guarantee.
| Selection Point | D703 | DD703 |
|---|---|---|
| Control concept | Non-CNC; the single controlled/servo axis is the Z-axis feed | CNC/multi-axis; marketed in the three-axis CNC range |
| Best starting point for | A simpler drilling configuration where the non-CNC positioning approach and controlled Z feed meet the job | Programmed coordinate positions, repeated hole patterns or a broader CNC positioning requirement |
| Current listed electrode range | φ0.3–φ3.0 mm | φ0.3–φ3.0 mm |
| Current listed X/Y travel | 300 × 400 mm | 350 × 450 mm |
| Current listed worktable | 480 × 360 mm | 450 × 350 mm |
| Current listed electrode/spindle servo stroke | 330 mm spindle servo stroke | 360 mm electrode servo stroke |
| Current listed maximum drilling thickness | Not published; confirm from the part and final quotation | 300 mm |
| Current listed maximum workpiece load | 200 kg | 200 kg |
| What still requires confirmation | Finished-hole size, depth capability, cycle time, accuracy, position, roundness, taper and surface condition for the actual material, electrode, flushing, settings and inspection method | |
Compare the full EDM hole drilling machine range, the single-axis EDM hole drilling category and the three-axis CNC EDM hole drilling category. Final selection should follow the visible machine definitions and the confirmed technical quotation.
What Are the Main Process Limitations?
- Conductivity is mandatory. A nonconductive material cannot be machined by this EDM process unless a different, specifically validated method is involved.
- Electrode diameter is not finished-hole diameter. The discharge gap, electrode wear, material, depth and settings influence the measured hole.
- Depth changes the process. Deeper holes can make debris removal and electrode wear more difficult, so no universal depth-to-diameter ratio should be promised.
- Accuracy requires a defined test. A table increment or programmed coordinate does not prove finished-hole size or position.
- Surface and metallurgical condition are application-specific. If recast layer, heat-affected zone, overcut, entry/exit condition, taper or roughness matters, state the acceptance rule and inspection method.
- Cycle time is conditional. Material, diameter, depth, flushing, electrical settings, electrode change and hole count all affect production time.
- Special features require confirmation. Blind holes, angled holes, automatic electrode changing, breakthrough detection and unattended automation must not be assumed from a generic EDM drilling description.
Information to Send for an EDM Drilling Review
A useful inquiry should allow the supplier to evaluate both physical machine fit and the required machining result. Send the following information:
- Workpiece material and exact grade, including heat treatment when relevant
- Part drawing, overall dimensions and weight
- Hole diameter, depth, quantity and through-hole or blind-hole requirement
- Hole coordinates, pattern, pitch, entry angle and available clearance
- Diameter, position, roundness, taper, surface or recast-layer acceptance requirements
- Required inspection method and sampling plan
- Production quantity, target cycle time and planned shifts
- Fixture, flushing and automation requirements
- Destination country, available voltage and frequency
If the smallest hole, deepest hole or most difficult material is critical to the purchase decision, provide that representative case first. HarsMarg can then review whether the published configuration is suitable, whether a sample test is appropriate and which conditions must be stated in the technical quotation.
Frequently Asked Questions
Can EDM drilling be used on nonconductive materials?
No. Standard EDM hole drilling requires an electrically conductive workpiece. Material names such as ceramic, glass or composite are not enough to establish suitability; the actual grade and electrical behavior must be reviewed.
Is the electrode diameter the same as the finished-hole diameter?
No. D703 and DD703 currently list a φ0.3–φ3.0 mm electrode-diameter range. Finished-hole size also depends on the discharge gap, electrode wear, material, depth, flushing and process settings. Quote the required measured hole diameter separately.
Can EDM drilling be used before Wire EDM?
Yes. Producing a start hole for threading the Wire EDM electrode wire is a common application. The start-hole diameter and position must match the following Wire EDM setup and programmed contour.
When should a buyer choose D703 instead of DD703?
Review D703 when a simpler non-CNC setup with controlled Z-axis feed meets the job. Review DD703 when programmed coordinate positioning or repeated hole patterns require a CNC/multi-axis configuration. Final selection must also consider travel, table area, workpiece load, drilling thickness, electrode range and the required result.
What accuracy or surface finish can EDM drilling achieve?
No single value applies to every material, diameter and depth. State the required hole size, position, form and surface acceptance together with the inspection method. The result should then be assessed for the selected machine, electrode, flushing arrangement and process conditions.
Can HarsMarg confirm cycle time from a hole diameter alone?
No. A useful cycle-time review also requires material grade, hole depth, quantity, pattern, electrode, flushing conditions, acceptance requirements and any electrode-handling or inspection time.
Request a Technical Review
Start with the HarsMarg EDM hole drilling machine range, compare the D703 single-axis machine with the DD703 CNC/multi-axis machine, and then send your drawing and application requirements. We will review the material, hole geometry, pattern, workpiece capacity, control needs and available power before preparing a technical quotation.
Table of Contents
- How Does EDM Hole Drilling Work?
- Common EDM Drilling Applications
- How Should You Choose Between D703 and DD703?
- What Are the Main Process Limitations?
- Information to Send for an EDM Drilling Review
-
Frequently Asked Questions
- Can EDM drilling be used on nonconductive materials?
- Is the electrode diameter the same as the finished-hole diameter?
- Can EDM drilling be used before Wire EDM?
- When should a buyer choose D703 instead of DD703?
- What accuracy or surface finish can EDM drilling achieve?
- Can HarsMarg confirm cycle time from a hole diameter alone?
- Request a Technical Review
