
 EN



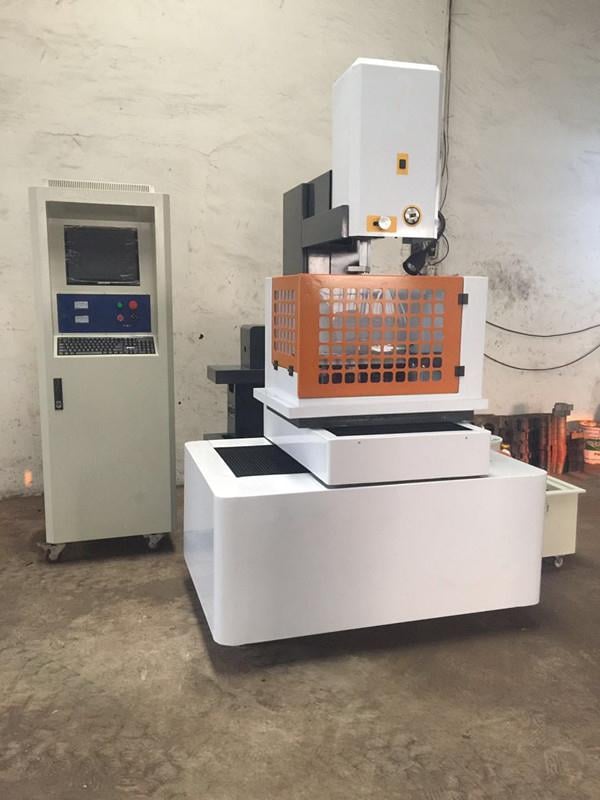
Automation changes how wire EDM equipment is prepared, run and recovered after a stop. Its value depends on the tasks the installed system actually performs. CNC programming, automatic wire threading, workpiece handling and remote monitoring are separate capabilities; a CNC label does not establish a fully automated production cell.
Separate the functions before comparing machines
Start with a written configuration list. Identify the controller and software version, which functions are included, which require options, and which belong to external equipment. Describe each task rather than accepting a general promise of intelligent automation.
- CNC programming defines the machining path and sequence. Ask how programs are prepared, checked and transferred.
- Gap or discharge control addresses the machining process. Confirm the documented feedback and adjustment functions; these do not establish automatic inspection of finished dimensions.
- Automatic threading and rethreading require a supported wire-handling system and recovery logic. Check starting conditions and the response when a retry fails.
- Automatic loading or fixture exchange requires a suitable handling arrangement and integration. Program transfer or networking alone does not move a workpiece.
- Monitoring reports the supported machine states or events. It does not by itself provide remote recovery, predictive maintenance or MES/ERP integration.
Define setup and recovery responsibilities
For a repeat job, specify who verifies the drawing revision, fixture, workpiece position, wire and cutting conditions before starting. A saved program can be part of the workflow, but it does not verify that the new setup matches the approved job.
Ask for a demonstration of the intended sequence, including operator actions. Where automatic rethreading is supplied, establish what happens after a wire break, repeated threading failure or another alarm. Do not assume that a machine can restart every interrupted job without checking its condition.
Treat unattended operation as a job-specific decision
A long automatic cutting cycle and unattended production are not equivalent. Before planning work without an operator present, confirm the manufacturer's instructions, required safeguards, consumable and maintenance needs, abnormal-stop behaviour and arrangements for responding to alarms. Validate the intended workpiece and setup rather than transferring another machine's operating claims.
Automatic control also does not replace part acceptance. Agree on dimensional and surface requirements, the measurement method and responsibility for checking the finished part. Machine-state information is not the same as measuring those results.
Evaluate the proposed workflow with accepted parts
Compare the existing and proposed workflows using the same part requirements and an agreed start and finish point. Record setup, operator attendance, cutting, stops, recovery, inspection and any rework within that boundary. Keep overlapping activities separate so elapsed time and labour time are not counted twice.
Report accepted output and the reasons for interruptions alongside time and cost. Separate estimates from measured results, and include software, handling equipment, integration, training and maintenance costs where applicable. More automation does not automatically mean a lower cost per accepted part.
Specify your requirements when requesting a quotation
When reviewing wire EDM equipment, send the material, drawing, thickness, workpiece size and weight, required tolerance and surface finish, batch size, power supply and destination country. Describe which tasks you want automated and when operator attendance is available. Request written confirmation of the proposed controller, options, integration responsibilities and acceptance procedure. Do not infer automatic threading, robotic loading or unattended capability from a product name.
Common questions about wire EDM automation
Does CNC control mean the machine has AI or a robot
No. CNC control, learning-based functions and robotic handling are different capabilities. Verify the supplied functions individually instead of treating the terms as interchangeable.
Does automatic threading guarantee continuous operation
No. The supported conditions, retry behaviour, maintenance and other interruptions still matter. Ask how the specific system stops, reports a problem and allows the job to be recovered.
Manufacturer documentation
For examples of the distinction between programming, discharge control and monitoring, see the FANUC ROBOCUT software overview. Mitsubishi Electric's MG-series development account discusses rethreading retries and maintenance-related stoppages. These documents describe those manufacturers' systems, not the supplied configuration of a HarsMarg machine.
Table of Contents
- Separate the functions before comparing machines
- Define setup and recovery responsibilities
- Treat unattended operation as a job-specific decision
- Evaluate the proposed workflow with accepted parts
- Specify your requirements when requesting a quotation
- Common questions about wire EDM automation
- Manufacturer documentation
