
 EN



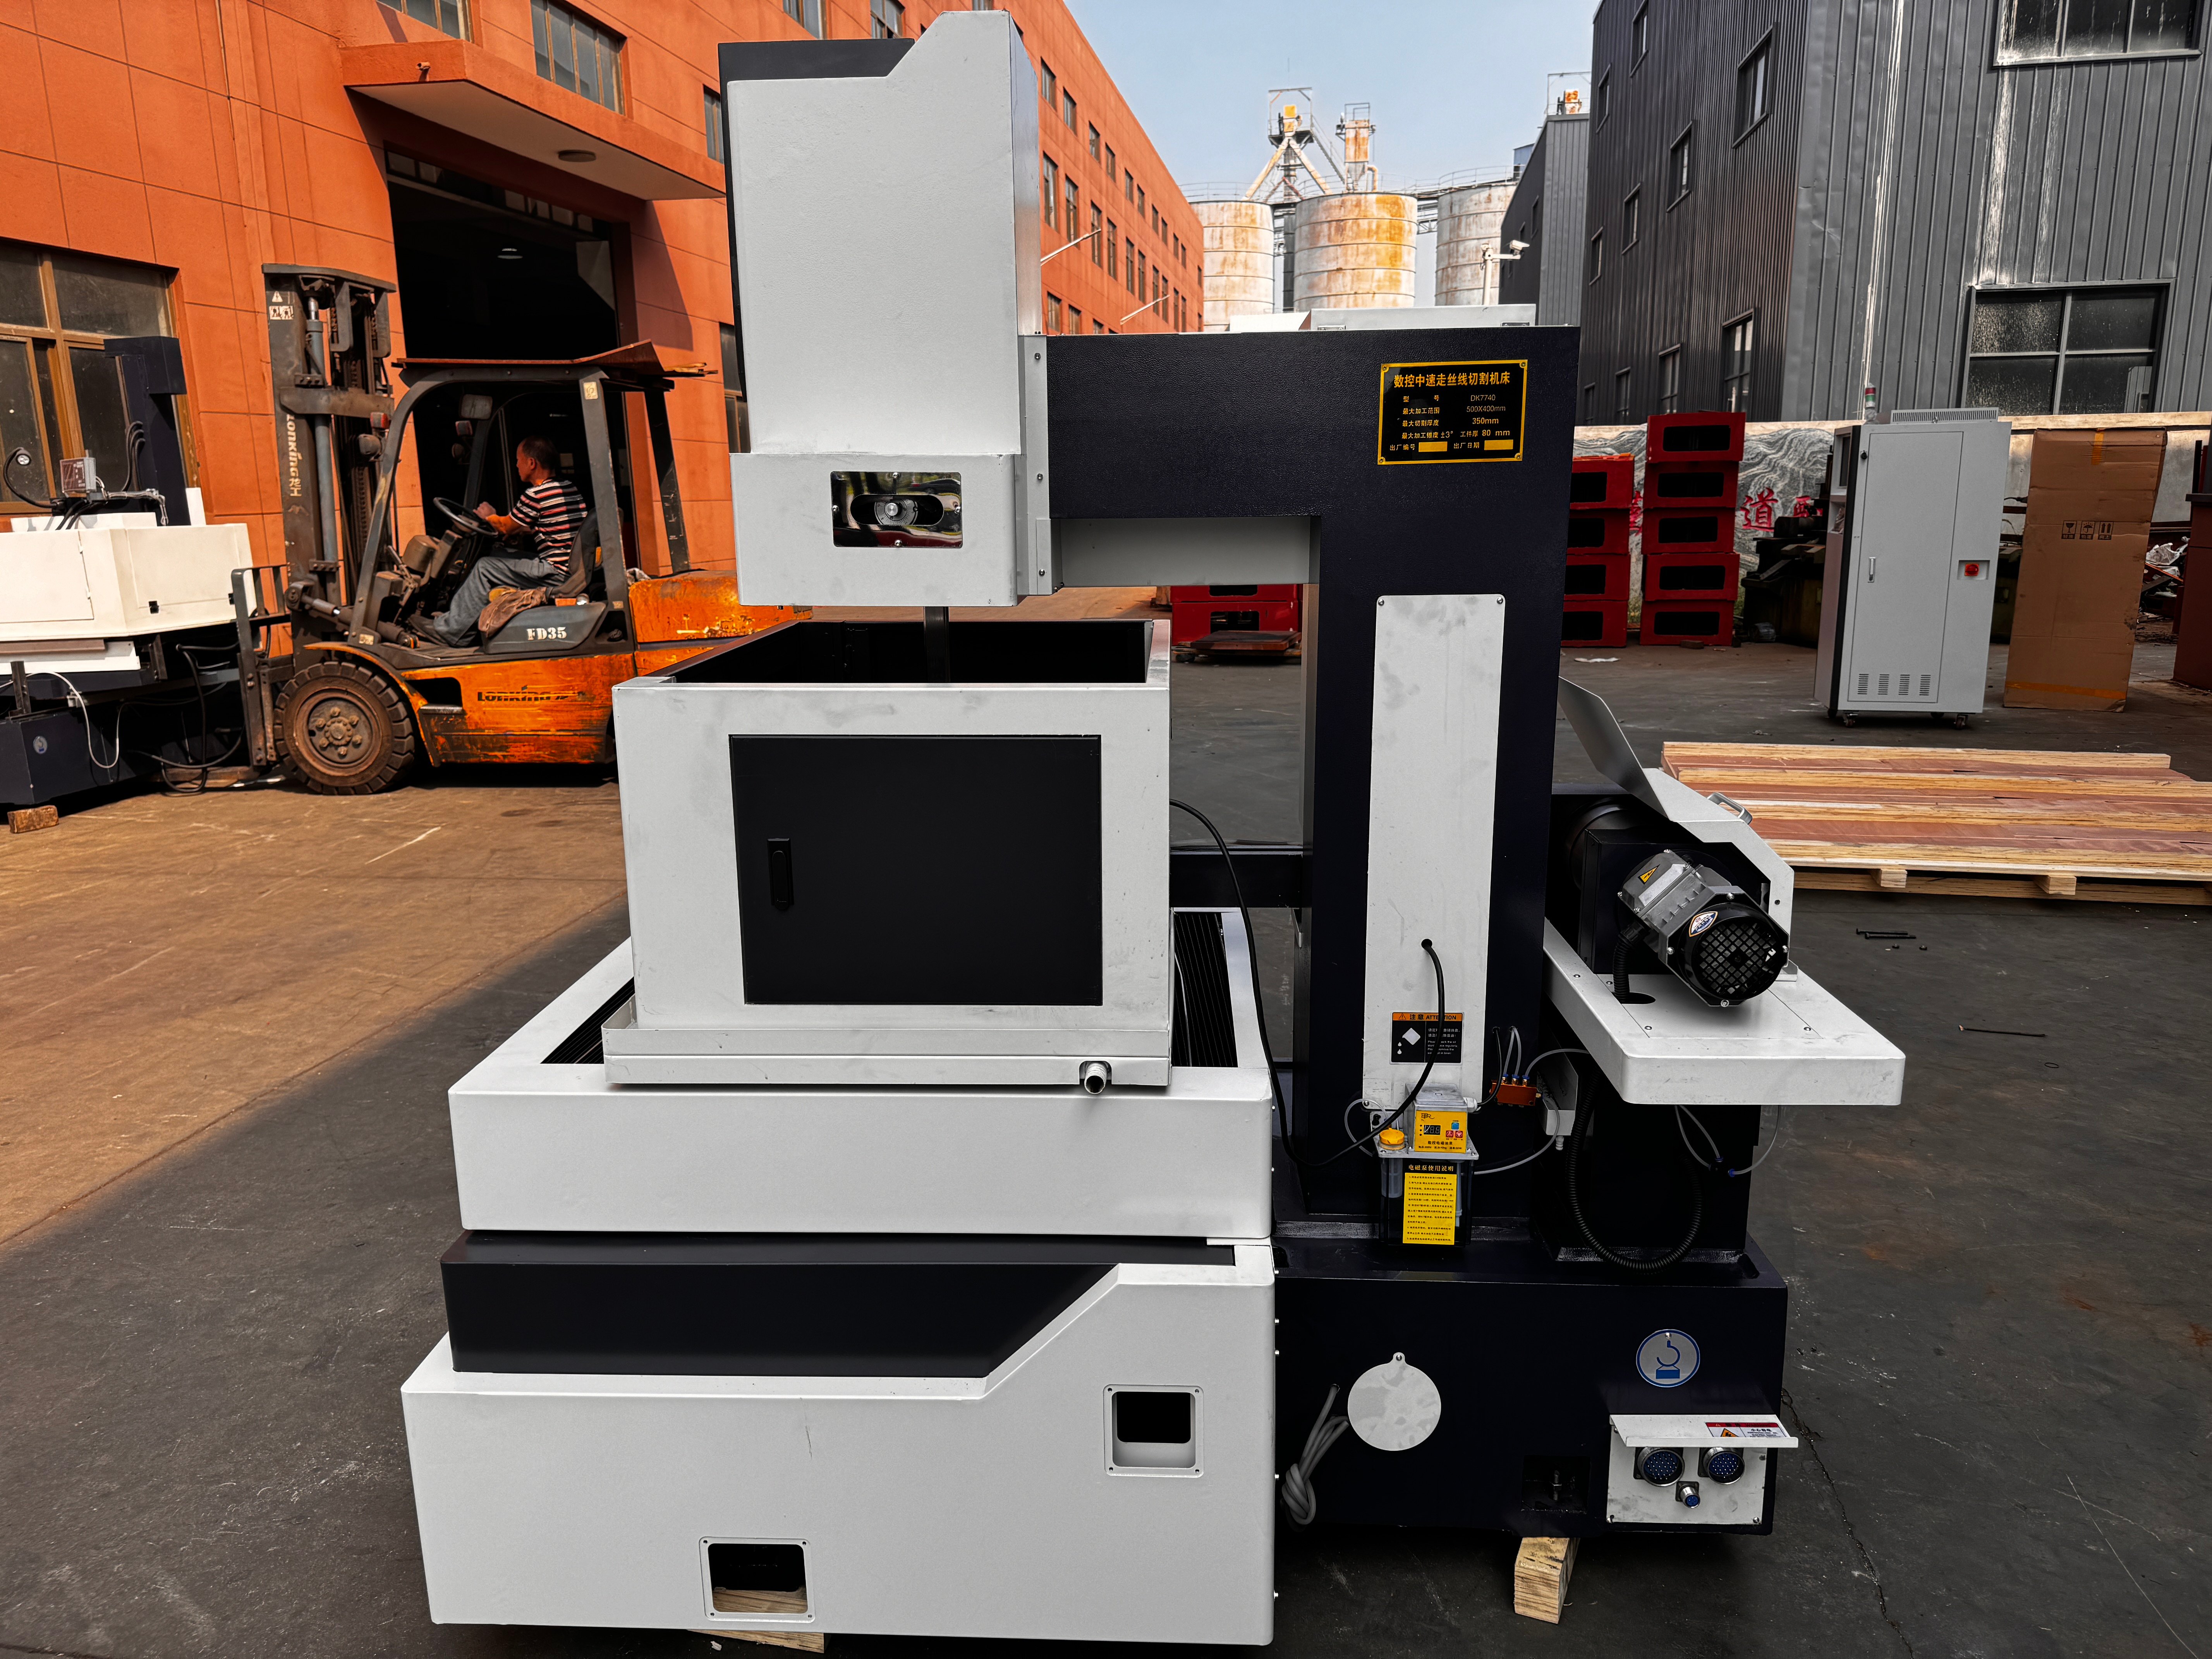
A better wire EDM surface finish starts with a stable cutting process, a suitable rough-and-trim strategy where the machine supports it, and a clear inspection requirement. There is no single roughness value that applies to every machine, material and cut stage.
Wire EDM removes material from an electrically conductive workpiece by spark erosion rather than a solid cutting edge. However, non-contact cutting does not mean a stress-free or thermally unaffected surface. Treat roughness, finished dimensions and any specified surface-integrity requirements as separate acceptance checks.
How Wire EDM Forms the Cut Surface
Discharge Craters and Surface Integrity
Electrical discharges locally melt and vaporize material, leaving overlapping craters. The size and distribution of those craters contribute to surface texture. Some molten material can resolidify as a recast layer; a low roughness reading alone does not prove that this layer is absent.
Use the machine manufacturer's cutting conditions as the starting point, not a generic recipe from another machine. Keep a record of the generator settings used for the actual material and thickness, and compare the resulting surface with the drawing requirement.
Rough Cutting and Trim Cutting
The main cut removes the bulk of the material. On a suitable multi-cut machine, trim cuts remove a controlled allowance using stage-specific offsets and settings. Appropriately chosen finishing discharges can form finer crater patterns and refine the texture. Measure the resulting roughness rather than inferring it from the number of passes.
Do not expect a fixed percentage improvement from each trim cut. Record the completed cutting sequence and inspect its result before adding another pass. A single-cut specification must not be presented as a multi-cut finishing capability without confirmation for the offered machine.
Wire and Operating Mode
Confirm whether the offered machine uses reciprocating reusable wire or continuous one-way wire. Select wire material, diameter and tension conditions for that machine and cutting stage. Do not assume that a description of brass-wire equipment also describes a reusable molybdenum-wire machine.
A finer wire is not, by itself, proof of a smoother surface. For each wire EDM model under consideration, ask which wire and finishing conditions support your drawing. Automatic tension control, automatic threading and active vibration compensation must be confirmed separately, not inferred from the equipment category.
Process Variables to Review
Pulse Settings and Cutting Stability
Pulse energy depends on voltage, current and pulse duration, not current multiplied by time alone. Finishing settings must also maintain stable discharge conditions; simply choosing the lowest available setting is not a complete finishing strategy.
Use the controller's documented parameter definitions and adjustment procedure. Record the starting settings, the reason for each change and the measured outcome. If short circuits or unstable cutting occur, investigate the process conditions rather than promising that automatic control will correct every defect.
Dielectric and Flushing Conditions
The dielectric electrically separates the wire and workpiece between discharges, helps the gap recover and carries heat away. Maintain its condition according to the offered machine's instructions. The required working-fluid system may differ between process families; there is no universal water-resistivity or filtration recipe for all machines.
Flushing carries eroded particles out of the cutting gap. Debris accumulation can disturb discharge stability, so review nozzle access, fluid condition and workpiece thickness. Include immersion where applicable. Follow the manufacturer's flushing recommendations and inspect the finished surface; a pressure value alone does not establish an acceptable finish.
Wire Travel Is Not Contour Feed
Wire travel describes movement of the electrode wire. Contour feed describes relative movement along the programmed workpiece profile. Record them as different variables. A statement about slowing the contour feed must not be translated into a blanket instruction to slow the wire-running system.
Inspect the actual cut at corners, transitions and other specified locations. An axis-positioning specification is not a roughness result or a finished-part guarantee. Where corner-control or compensation functions are proposed, confirm their availability and assess the completed feature against the drawing.
Material and Geometry Define the Trial
State the Actual Material
Provide the material grade, heat-treatment condition and any relevant coating or prior processing. Do not rank achievable finish from thermal conductivity or hardness alone. A successful result on one alloy is not evidence that the same settings will meet the requirement on another.
If the drawing specifies recast-layer limits, microcracks or another surface-integrity condition, agree how that condition will be examined. Keep this separate from the Ra requirement. No generic surface-finish article can qualify an aerospace, medical or other critical component for use.
Choose a Representative Cut
Describe the section thickness, cut length, taper, corners and narrow features that matter on the real part. Agree which features a trial must represent. A convenient straight cut should not be used as proof of finish on every difficult feature of a different workpiece.
Mark where measurements are required, including different heights or contour locations if the drawing calls for them. Check access for flushing and inspection before accepting the trial plan. The report should identify the measured areas rather than imply that the whole surface has been verified.
Confirm the Offered Machine Configuration
Generator and Multi-Cut Support
Ask for the exact machine model, controller and generator configuration. Identify which cutting stages and parameter sets are supported. A feature shown in a high-end manufacturer's catalogue does not establish that it is included in every Wire EDM machine.
List standard functions, optional functions and functions not included in the quotation separately. If automatic switching between cutting stages is requested, have the supplier describe how it works on the offered configuration. Do not substitute a generic claim about adaptive control for that explanation.
Wire Guidance and Maintenance
Review guide condition, alignment, wire support and the relevant maintenance procedure. Record the actual tension setting or adjustment method used in a trial. Do not describe manual adjustment as closed-loop tension control or infer a guide-position accuracy from the name of its material.
Where automatic tensioning or vibration compensation is offered, request the specific configuration and operating instructions. Establish its role in the proposed cut, then inspect the result. The presence of a control function is not a replacement for surface or dimensional acceptance.
Monitoring and Finished-Surface Measurement
Gap-voltage or discharge-current information can help evaluate cutting stability. It is not, by itself, a measurement of Ra or proof that a recast-layer requirement has been met. Keep process observations and finished-surface inspection results distinct in the trial record.
Do not assume that AI adjustment, optical roughness inspection or predictive maintenance is installed. If any such function matters to the purchase, request a model-specific description of its scope and limitations. Avoid treating an unverified feature as a promise of defect-free production.
Define Acceptance Before Comparing Results
Specify the Roughness Measurement
Ra describes the arithmetic mean of absolute profile-height deviations; it is not interchangeable with Rz or the areal parameter Sa. State the required parameter and unit on the drawing or inspection agreement, rather than asking only for a smooth or mirror-like surface.
Agree the instrument, applicable measurement standard, filtering, evaluation length, measurement direction and locations. Use appropriate calibration and record the measurement conditions. Compare results obtained under a compatible method; a photograph or a roughness number without its conditions is not sufficient acceptance evidence.
Match Finishing Effort to the Drawing
Identify the surfaces that need finishing and the required cutting sequence. Compare complete cycle time with the measured result, not an assumed improvement per pass. Additional cuts can add time without automatically satisfying every roughness, dimensional or surface-integrity requirement.
For a technical machine review, provide the drawing, material and thickness, target roughness and tolerance, required quantity, power supply and destination country. Identify any requested automation separately. Ask which configuration and trial conditions can be proposed before accepting a performance commitment.
Plan Any Post-Processing
If polishing, grinding or another finishing operation is required, include it in the process and inspection plan. Define when the specified dimensions and surface condition must be checked. Do not promise that removing surface material will leave every dimension or edge unchanged.
A trial report should identify the machine, wire, material, geometry, cut stages, fluid conditions and measurement method. Label a trial result as a result under those conditions, not as a universal capability. Keep any additional qualification requirements tied to the customer's specification.
FAQ
What Surface Roughness Can Wire EDM Achieve?
There is no reliable universal value for all machines and materials. Ask for a model-specific result that identifies the material, thickness, wire, cutting sequence and measurement conditions. Do not substitute an axis-positioning figure, a competitor's result or an unspecified mirror-finish claim for that evidence.
Is Wire EDM Always Smoother Than Grinding or Milling?
No universal ranking is justified. Compare the finished surface and dimensions required by the drawing, including any relevant surface-integrity criteria. Different processes and finishing sequences should be assessed against the same acceptance requirement, rather than selected from a general claim of superior finish.
Can Different Features Receive Different Finishing Treatments?
Identify the critical features and ask whether the offered controller, toolpath and setup support the required treatment. Do not assume that finish requirements can be switched automatically on every machine. Confirm the practical cutting sequence and inspect the specified features after processing.
Where Should a Surface-Finish Investigation Start?
Check the measurement method first, then review material identification, cutting stages, settings, fluid conditions and wire-guidance condition. Record a controlled adjustment and inspect its outcome. If the requirement is still unmet, reassess the trial and machine configuration instead of promising a single universal fix.
