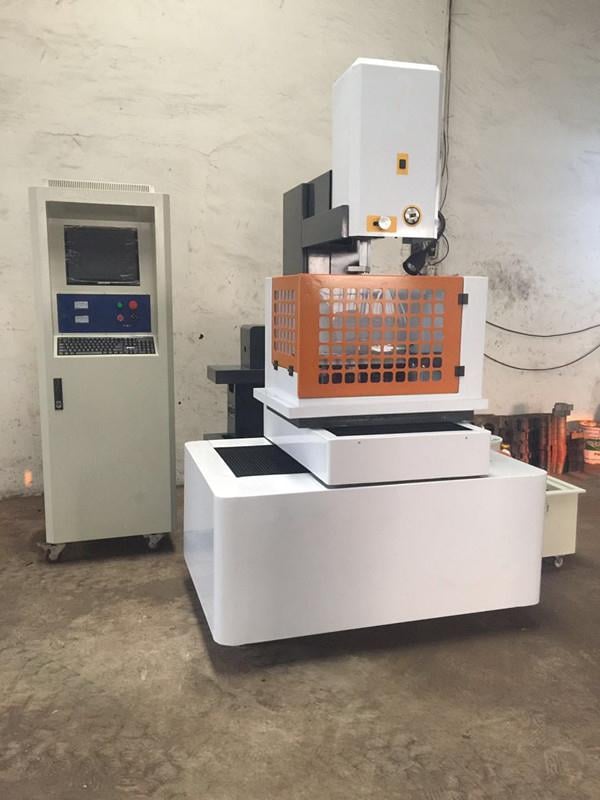
Automation changes how wire EDM equipment is prepared, run and recovered after a stop. Its value depends on the tasks the installed system actually performs. CNC programming, automatic wire threading, workpiece handling and remote monitoring are sepa...
VIEW MORE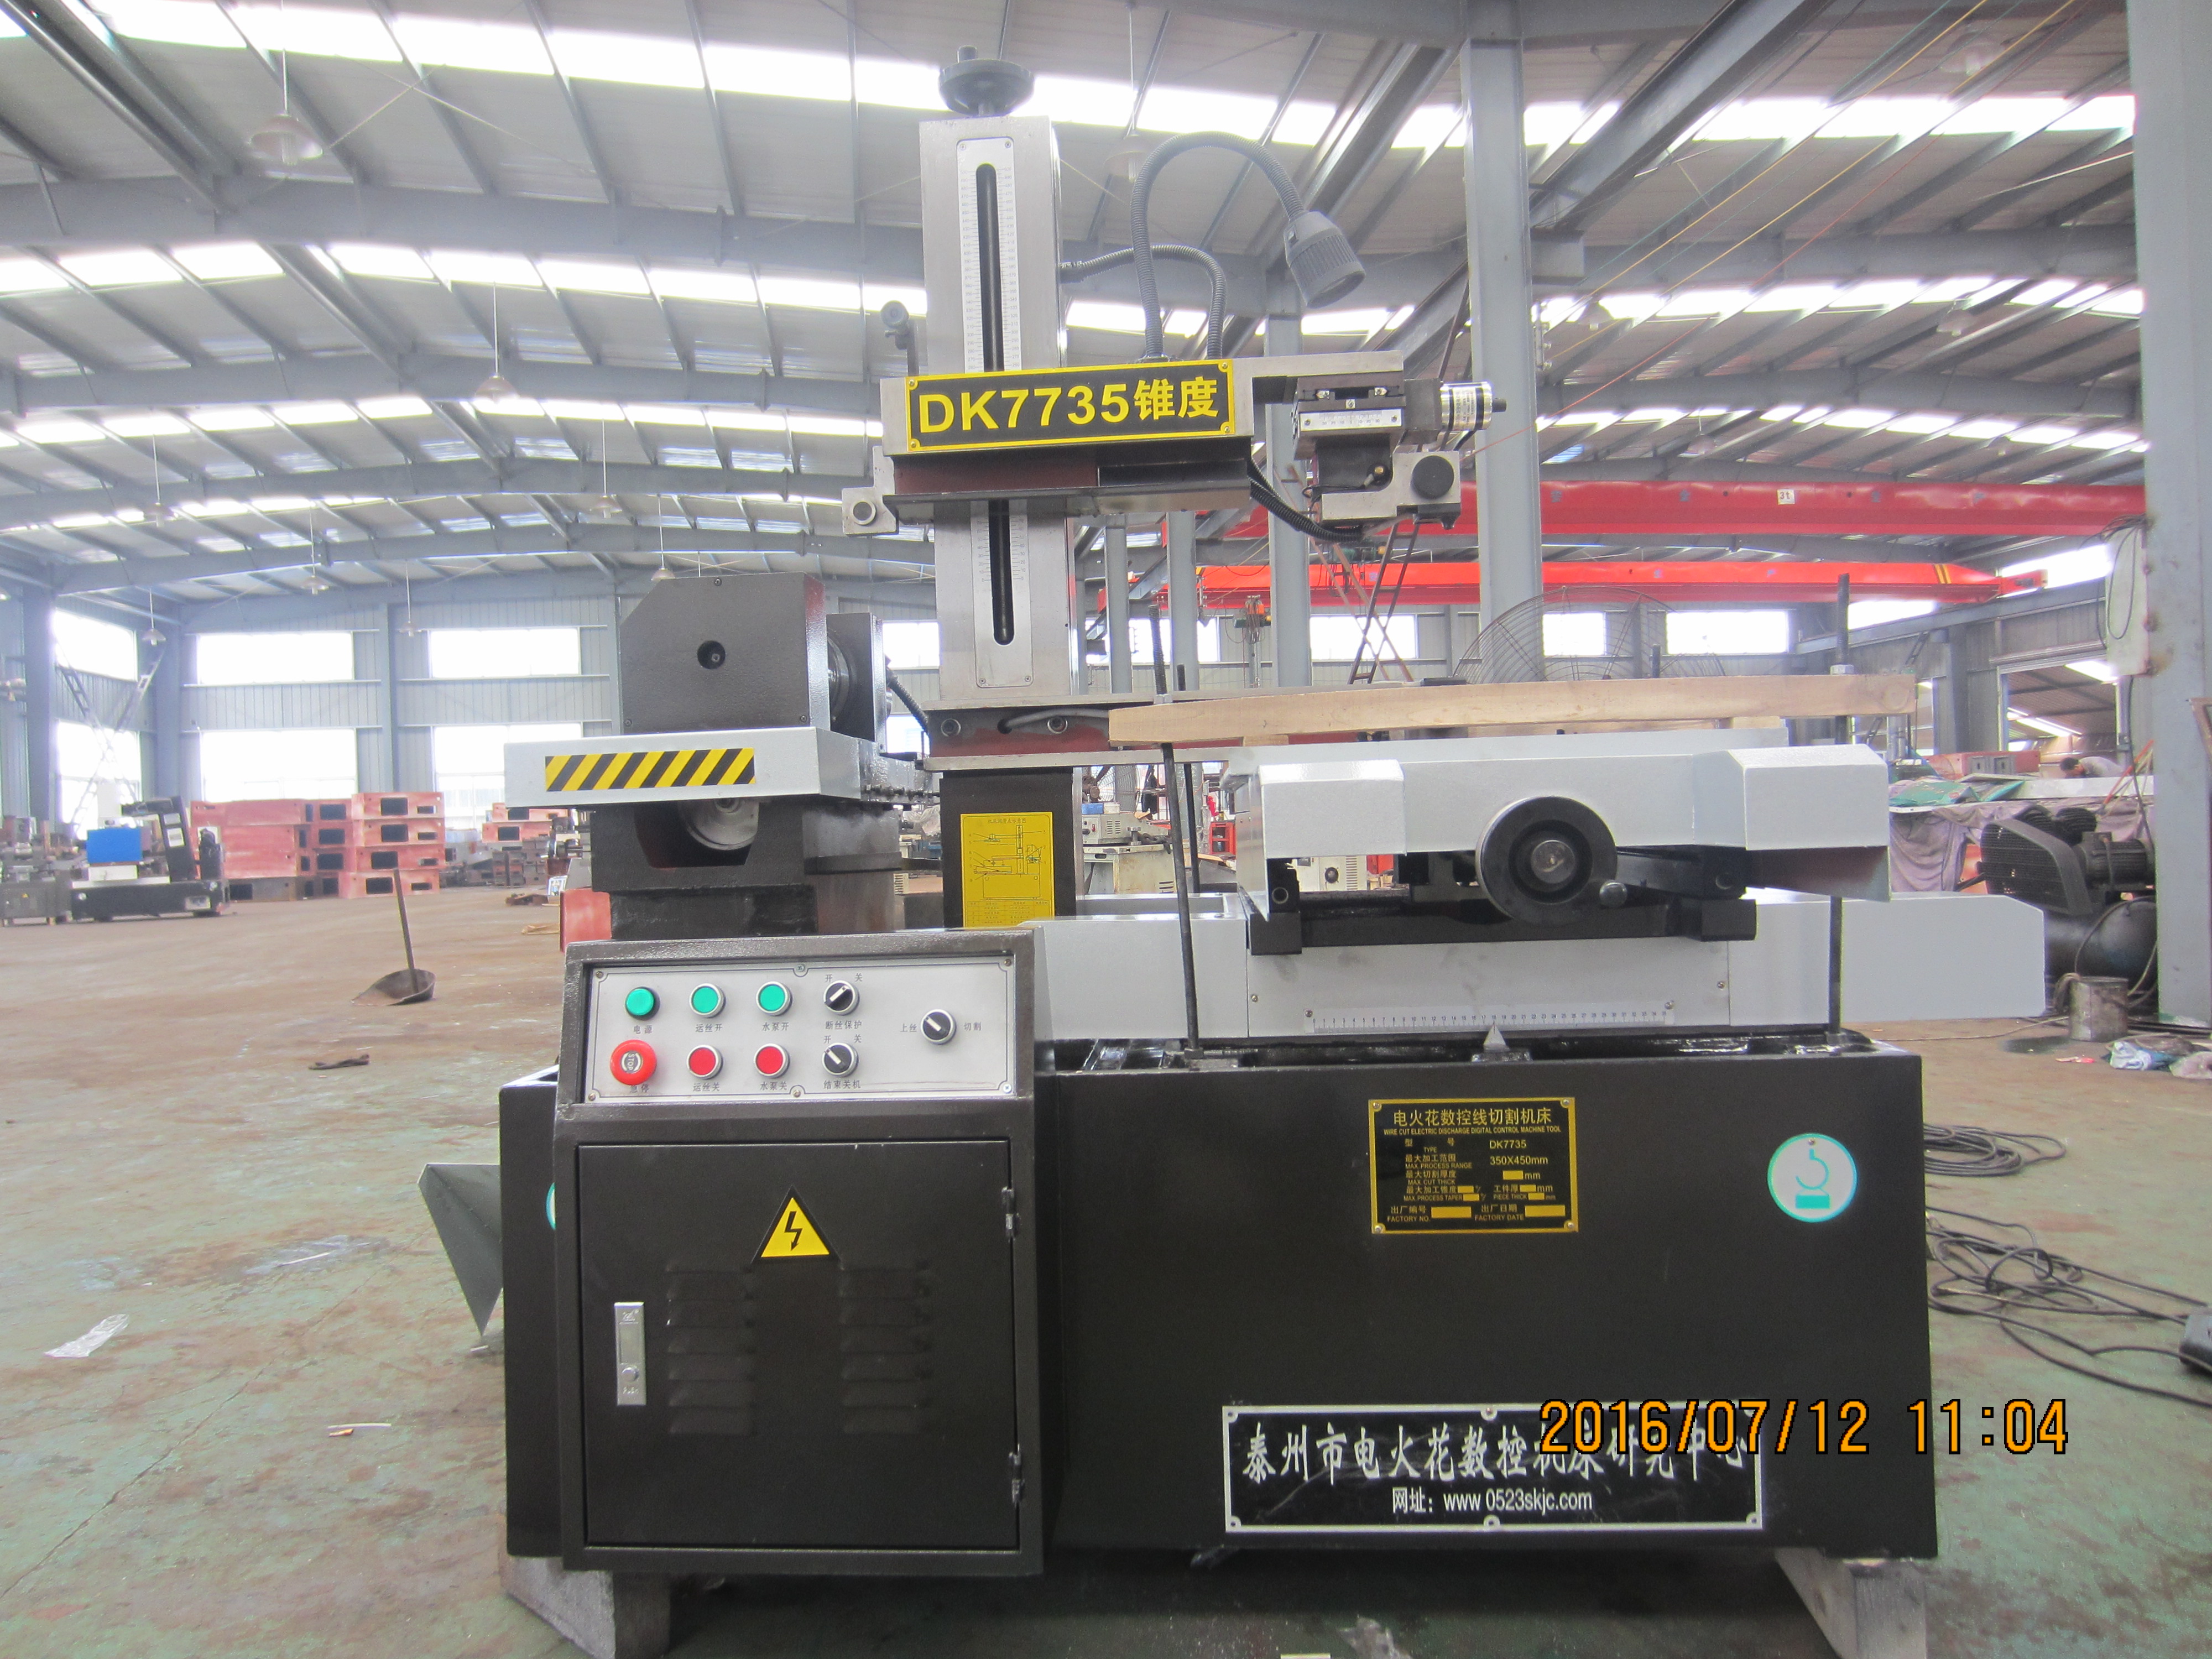
For HarsMarg single-cut and multi-cut Wire EDM machines, extending wire life means keeping the reusable molybdenum wire and its complete reciprocating transport system in a stable, serviceable condition. Inspect the wire, drum winding, reversal, tens...
VIEW MORE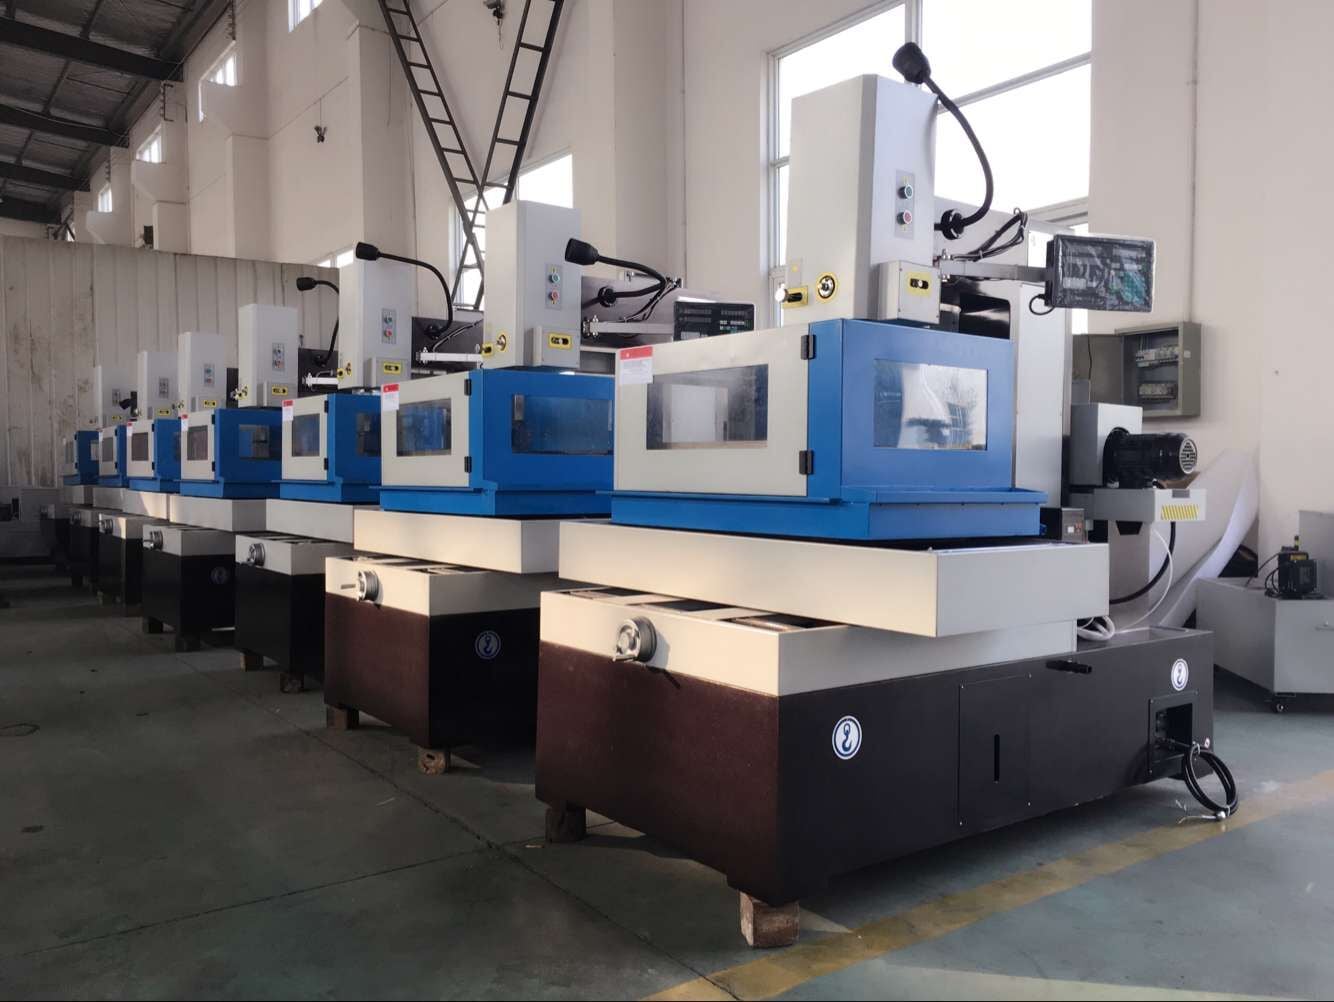
Consistent EDM performance comes from controlling the same inputs every time: the machine condition, working fluid, consumables, setup, electrical program, environment and inspection method. When cutting time, surface finish or dimensions begin to dr...
VIEW MORE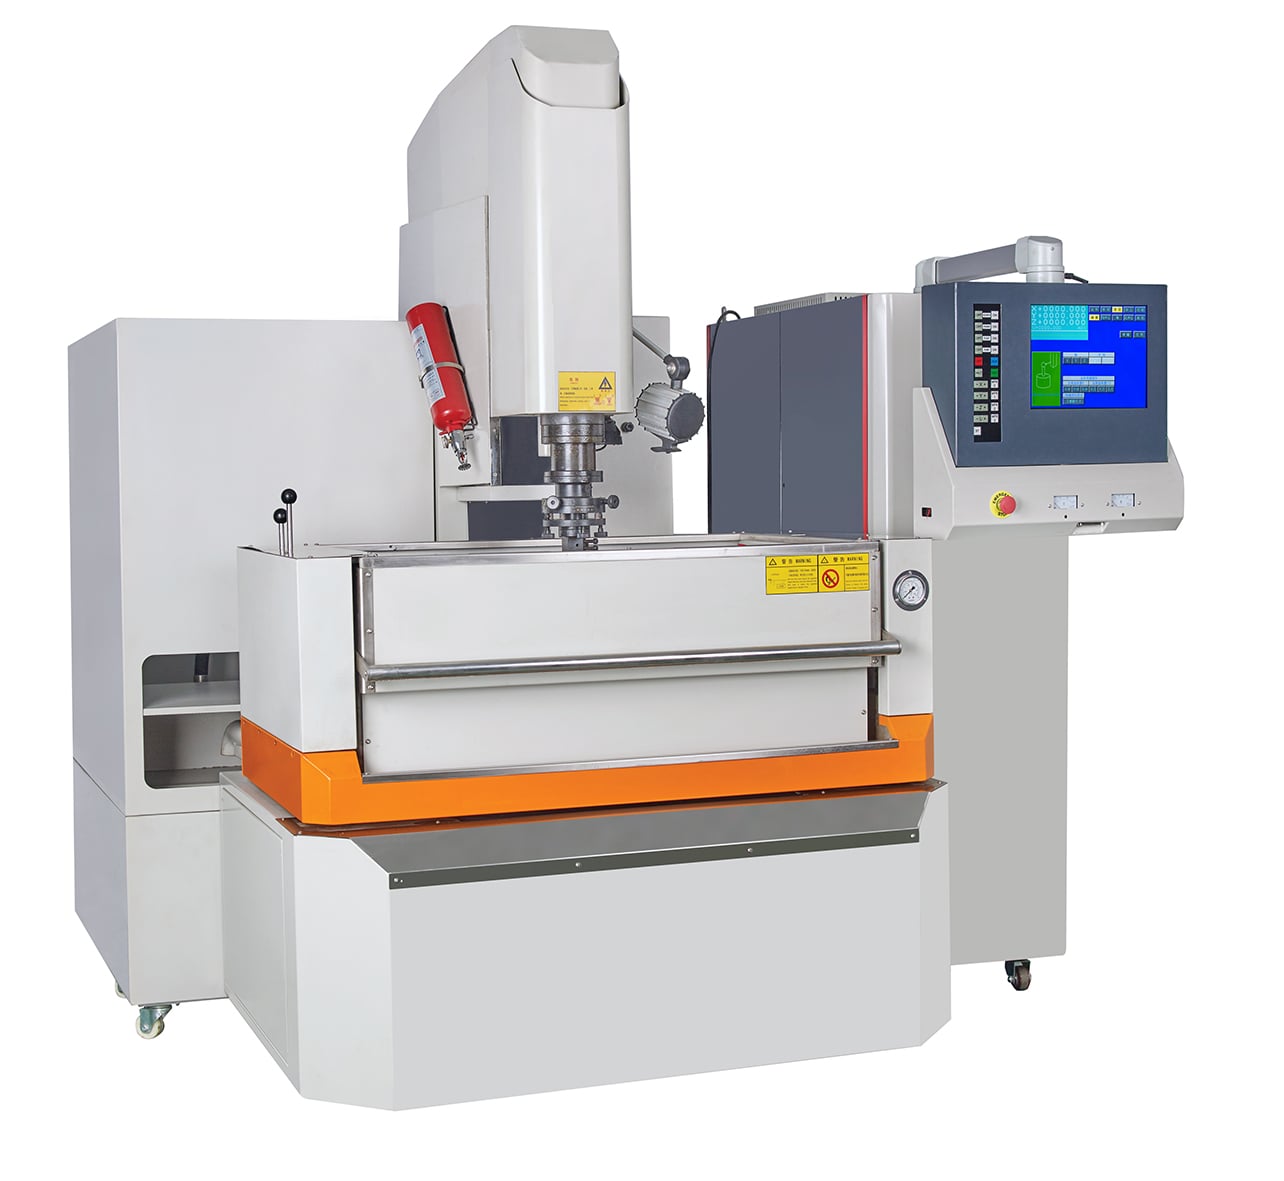
Sinker EDM machines form cavities in electrically conductive workpieces using a shaped electrode and controlled electrical discharges. For a mold cavity, useful accuracy starts with a defined drawing, a feasible electrode approach and an inspection p...
VIEW MORE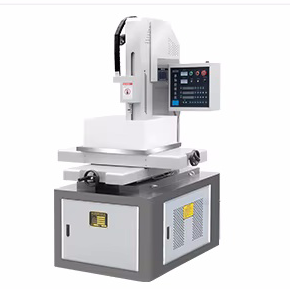
Small hole drilling represents one of the most challenging manufacturing processes in modern industry, demanding exceptional precision and specialized techniques to achieve consistent results. This manufacturing process involves creating holes with d...
VIEW MORE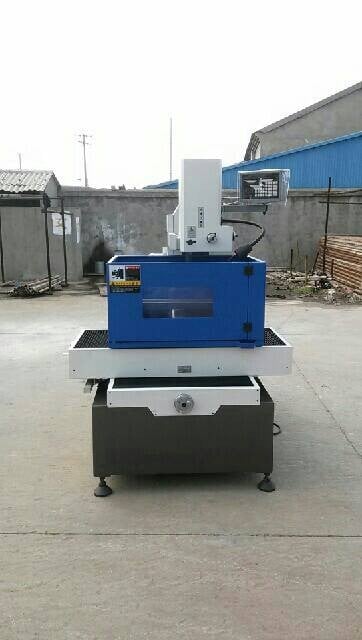
On HarsMarg machines, both fast-wire and medium-speed Wire EDM use a reciprocating, drum-stored molybdenum wire. The practical difference is the cutting sequence. The fast-wire range is positioned for single-cut machining, while the medium-speed rang...
VIEW MORE
Wire EDM and laser cutting are both thermal, non-contact cutting processes, but they qualify a part in different ways. Start with Wire EDM when the workpiece is sufficiently conductive and the required contour can be produced by a wire passing throug...
VIEW MORE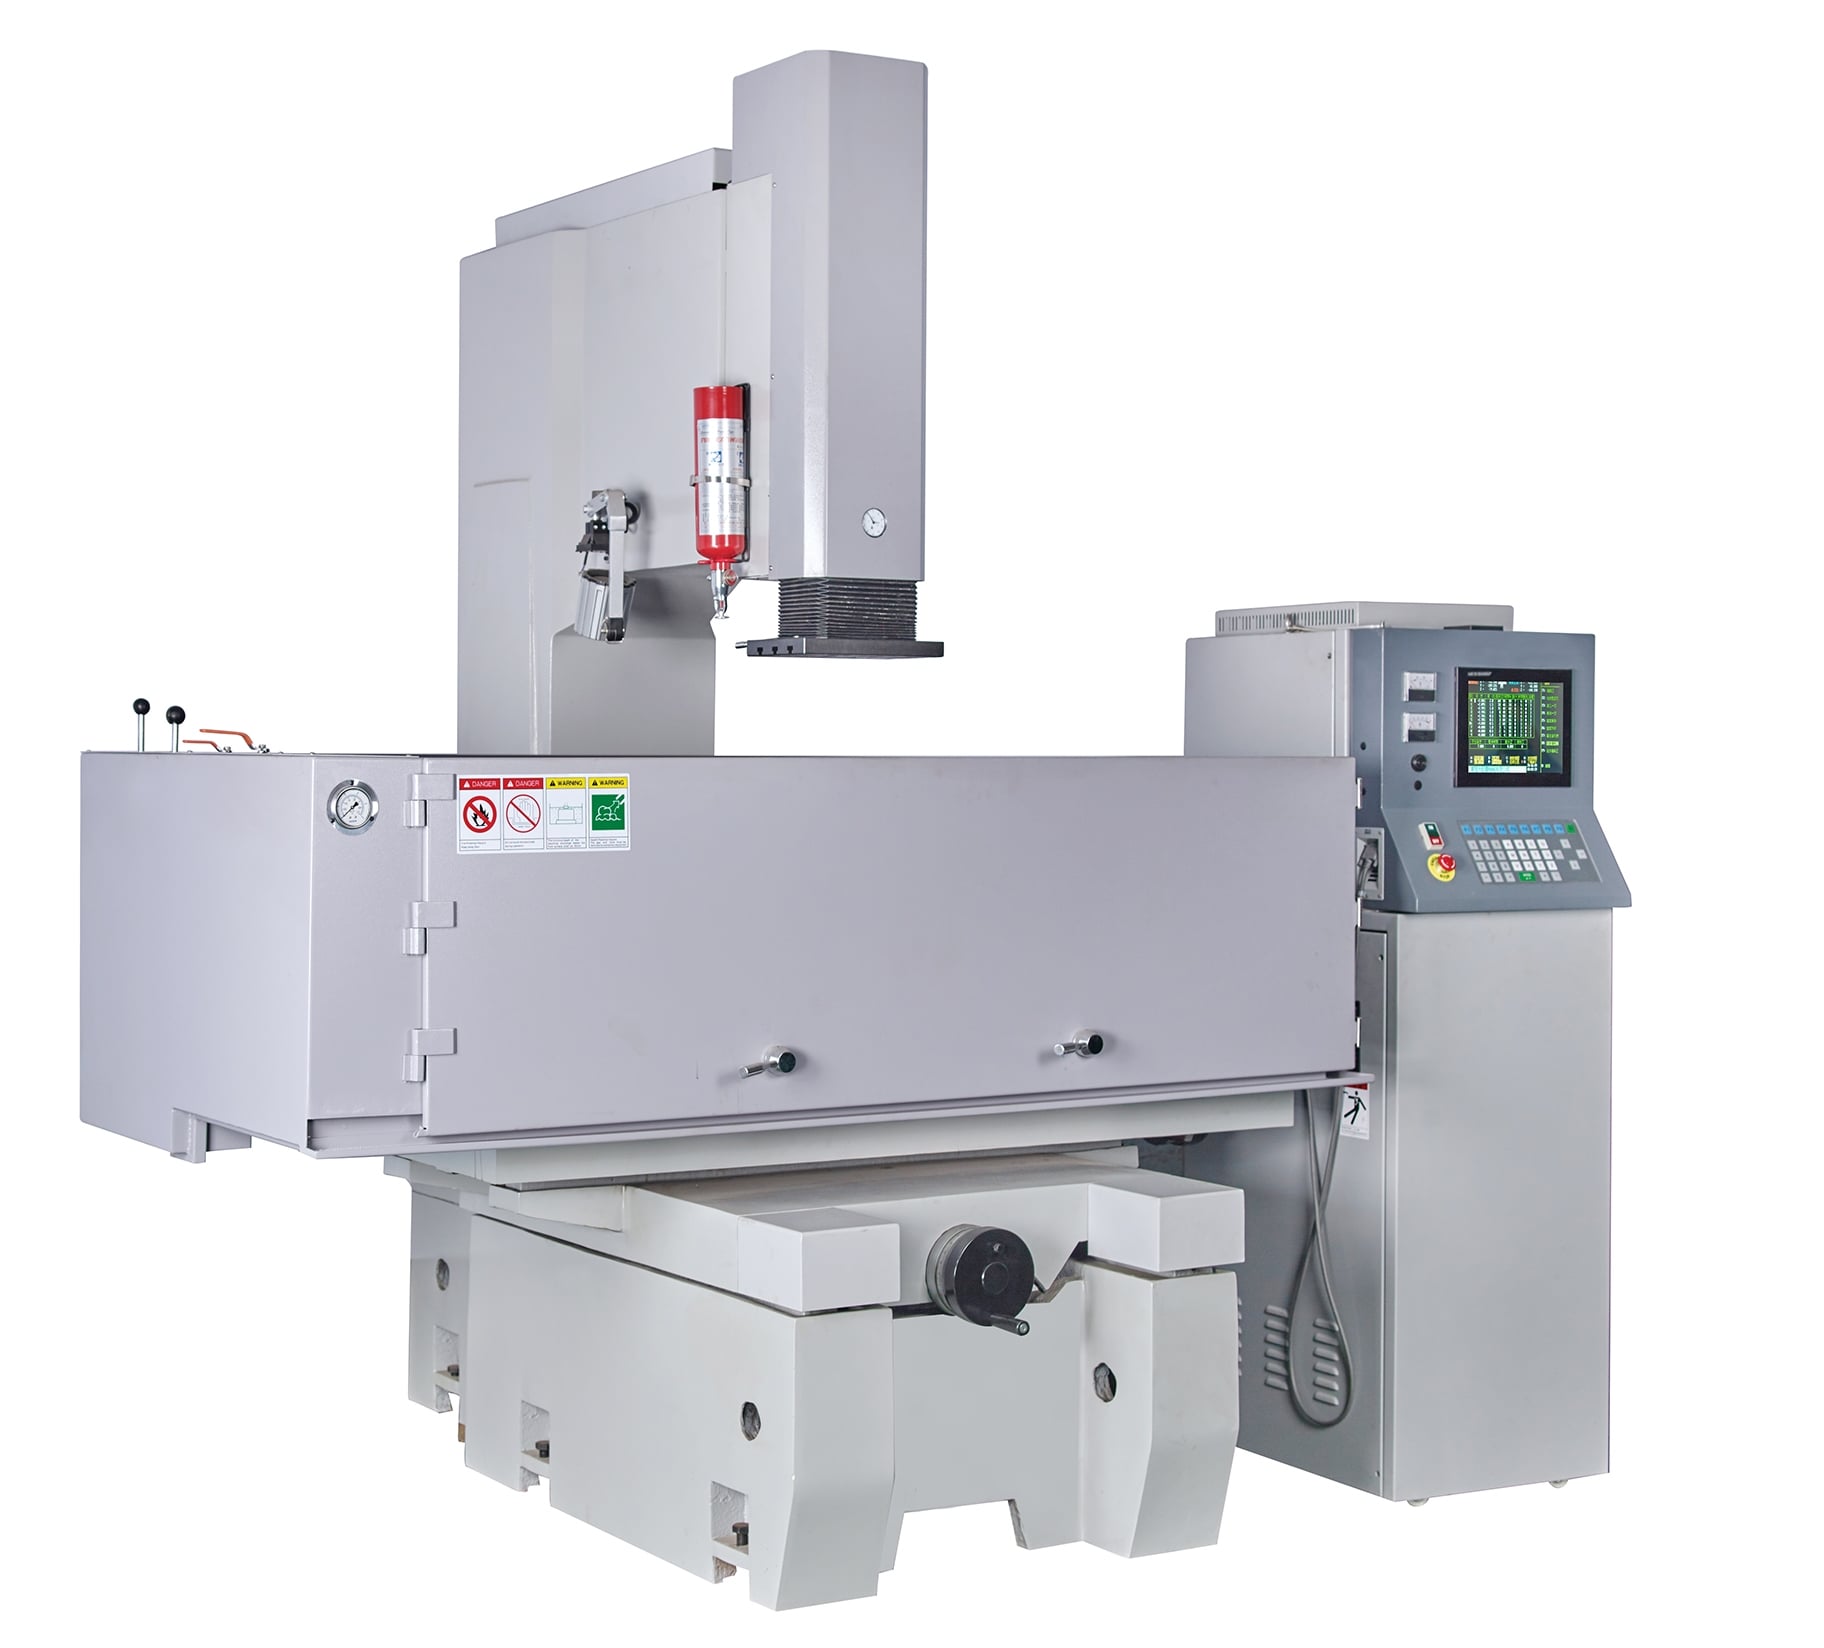
sinker EDM can help a mold project when it solves a cavity feature that is difficult to produce by milling alone. It does not automatically shorten every job. Evaluate the complete route: electrode preparation, setup, roughing and finishing burns, in...
VIEW MORE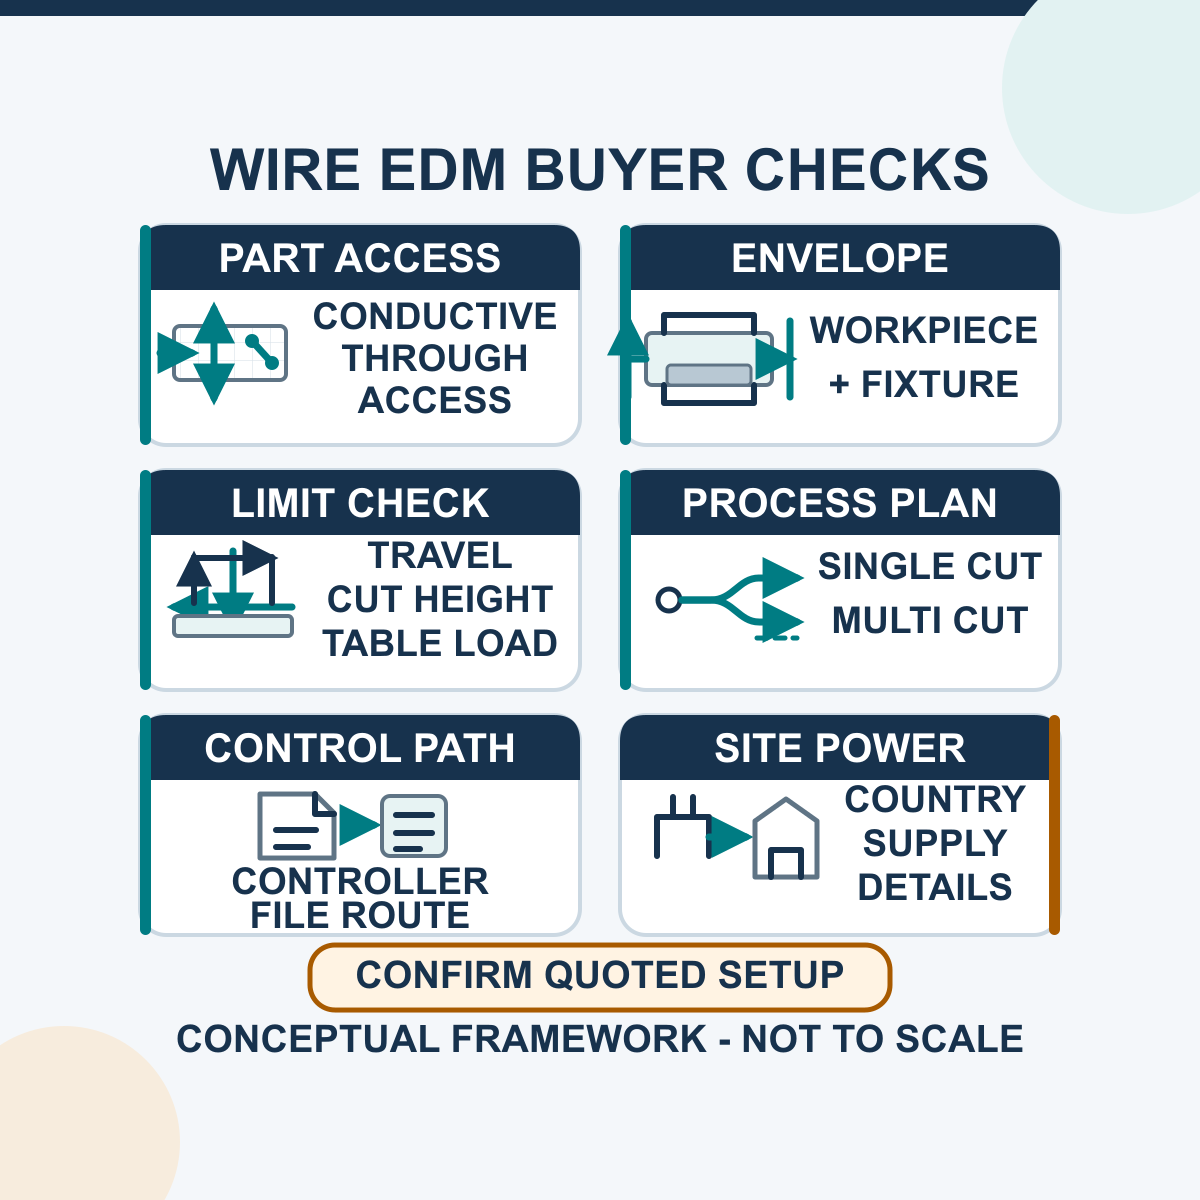
Choose a Wire EDM machine by starting with the part, not with a machine label. First confirm that the workpiece is electrically conductive and that the required profile can be cut through the material from an edge or a prepared start hole. Then match...
VIEW MORE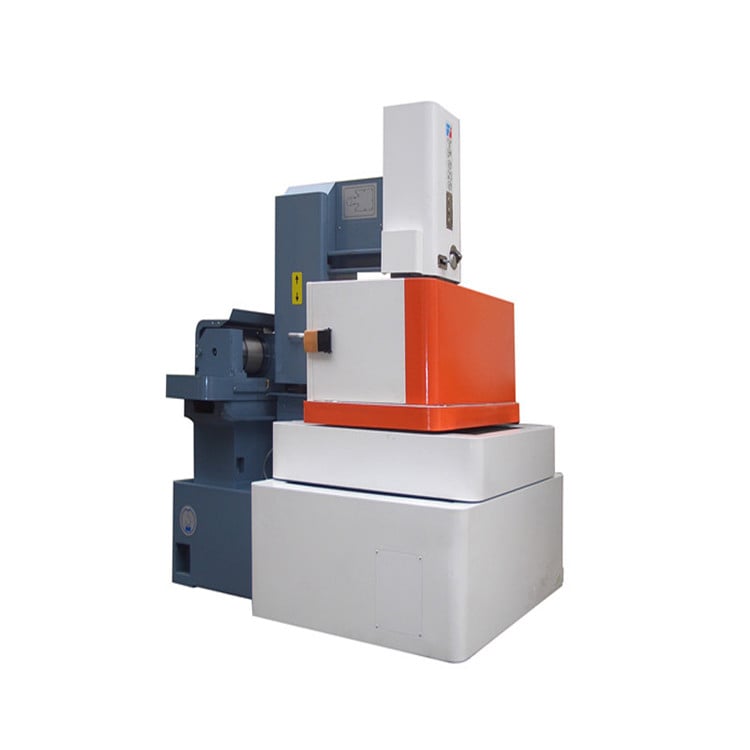
Improving productivity with EDM machines starts with the number of accepted parts completed over the full job, including preparation, machining, interruptions and inspection. Identify the actual bottleneck before changing a process. Compare candidate...
VIEW MORE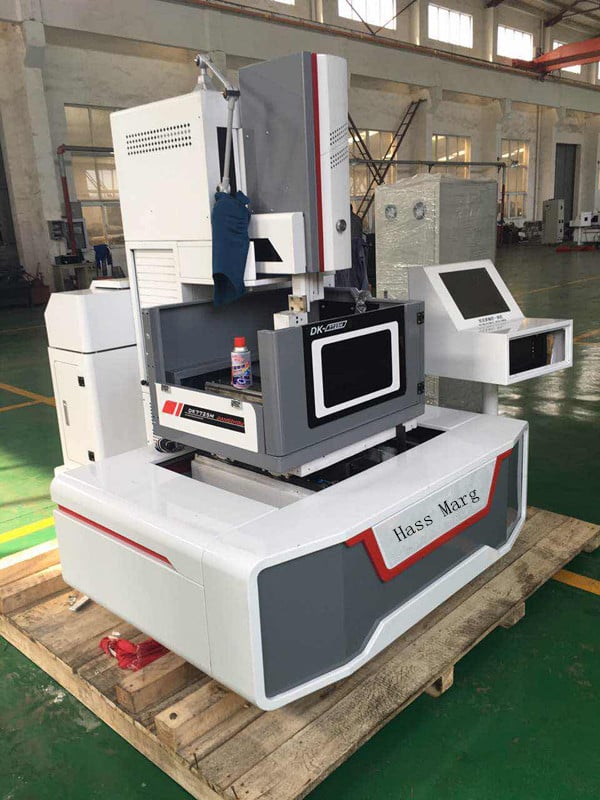
Wire EDM is most useful when a buyer needs a precise through-profile in an electrically conductive material, especially after the workpiece has been hardened or when conventional cutting force could distort a delicate feature. It can produce complex ...
VIEW MORE
Safe Wire EDM operation starts with the instructions for the exact machine, not a generic voltage, fluid-change interval or PPE list. Before cutting, the operator should confirm training and authorization, guards and interlocks, emergency controls, w...
VIEW MORE
 EN



